

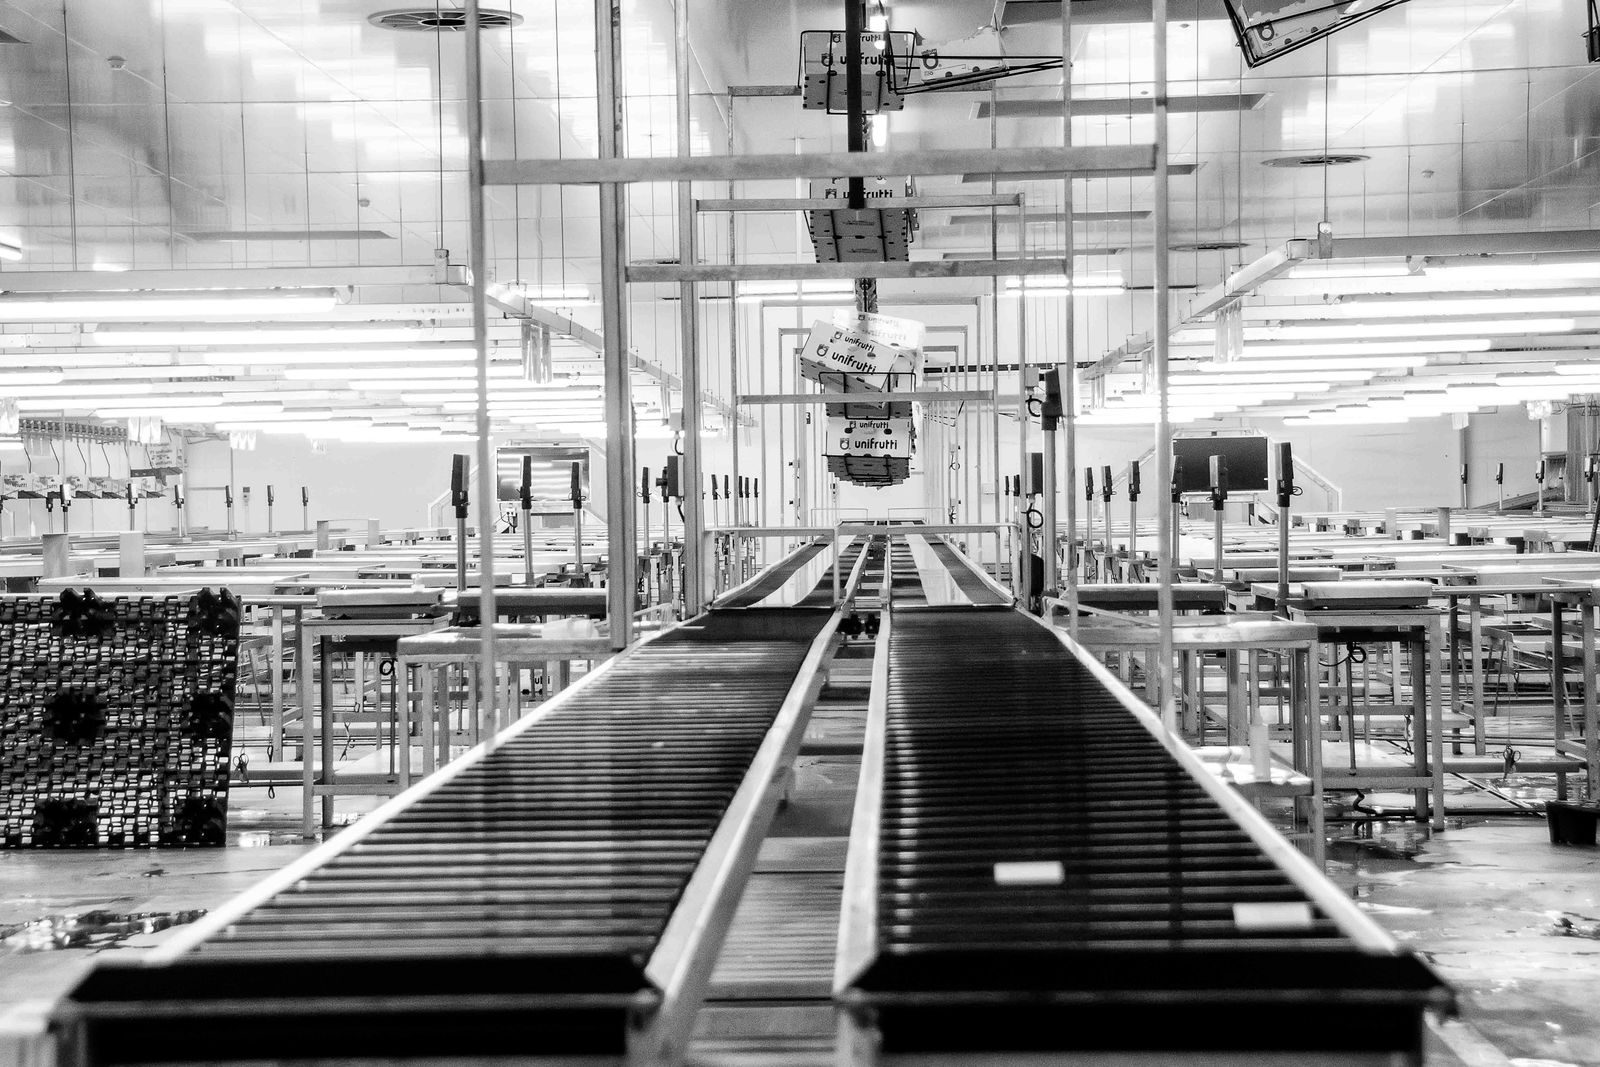
Every conveyor is essentially a transport question: what are you moving, how far, how fast, and under what conditions? Begin by defining the product load—weight per unit, dimensions, surface type, and whether it is loose, packaged, or palletized. A belt conveyor suits uniform boxes and bags, while a roller conveyor handles rigid pallets and totes. For bulk powders or granules, screw or chain conveyors are the usual answer.
Temperature, humidity, dust, and chemical exposure change the required materials and motor rating. Food-grade and pharmaceutical applications need stainless steel frames and wash-down motors. Heavy manufacturing environments demand sealed bearings and impact-resistant belting. If the line runs near ovens, freezers, or chemical baths, specify temperature-rated components from the start rather than retrofitting later.
Calculate the required units per minute or mass flow rate, then add a 15–20% growth margin. Map the route: horizontal runs, inclines, declines, curves, and transfers. Each change in elevation or direction reduces effective capacity and may require side guides, cleated belts, or vacuum sections. Keep the path as straight and level as possible to minimize drive power and maintenance.
The cheapest purchase price is rarely the lowest lifetime cost. Look at energy consumption, belt/roller replacement intervals, spare-part availability, and ease of access for cleaning and service. A modular design with standard components shortens downtime and makes future expansion easier.
The three conveyor families behave differently under load, and the wrong choice usually shows up as jams, spillage, or premature belt wear rather than as an obvious failure. Start by asking what the load rests on and how it has to be restrained.
| Type | Best for | Watch out for |
|---|---|---|
| Belt | Uniform boxes, bags, parcels, and loose parts carried on a continuous surface | Belt tracking drift on long runs; edge wear at transfers |
| Roller | Rigid pallets, totes, and drums with a flat, firm base | Soft or uneven bottoms that bridge between rollers and stall |
| Overhead or monorail | Freeing floor space and moving loads between levels | Higher structural load on the building; harder access for maintenance |
| Screw or chain | Bulk powders, granules, and hot or abrasive material | Limited length per drive; trough abrasion with abrasive media |
A conveyor is only as good as the control layer behind it, so decide early whether the line simply transports product or has to make decisions about it. Once scanners, diverters, and merge points enter the design, throughput is governed by the control logic and the scan window rather than by belt speed alone. Lines that must divert, merge, and route to individual destinations are designed around sortation and parcel sorting automation rather than around a single conveyor.
Mechanical fabrication matters just as much. Frames, guards, and support structures are cut, formed, and welded from steel, and repeatability between modules depends on how accurately those parts are produced. Laser cutting and welding equipment is what lets a fabricator hold the same dimensions across a run of identical frames instead of re-fitting every module by hand.
Confirm the interfaces before ordering: motor starter and VFD ratings, emergency-stop architecture, PLC and network protocols, and how the line hands off to the next process or to a warehouse management system.
Most conveyor problems that reach the maintenance log were decided on the specification sheet, long before anything was built.
| Mistake | What it leads to |
|---|---|
| Sizing for today's throughput with no growth margin | A line that is at capacity the day it is commissioned |
| Designing to the fastest station instead of the slowest transfer | Bottlenecks at merges, transfers, and inclines |
| Choosing the drive before the load is known | Underpowered starts, slipping, and motor overheating |
| Leaving no access for cleaning and service | Longer planned stops and more unplanned downtime |
| Ignoring accumulated product during an emergency stop | Spillage, damage, and jam clearance that blocks the line |
The fastest route to a quotation you can compare against others is to send four things: a description of the load including unit weight, dimensions, and the condition of its base; the required throughput in units or tonnes per hour; a layout sketch with available floor space and ceiling height; and the environment the line will run in. With those four, an engineer can propose a type, a belt or roller specification, and a drive arrangement. Without them, every supplier will quote a different machine and the prices will not be comparable.
Ask what the product rests on. If it can span two support points without sagging, a roller conveyor is usually cheaper to run and easier to accumulate on. If it is loose, flexible, or irregular in shape, a belt carries it more reliably.
A common starting point is 15 to 20 percent above current peak throughput, but the honest answer depends on how predictable your demand is. Margin you never use is capital tied up in wider belts and larger drives.
Usually, if the existing control architecture is documented. The constraint is rarely floor space; it is whether the existing PLC, safety circuit, and network can accept another node without a redesign.
At ZH Industrial Machinery, we size and configure industrial conveyor systems around real production data. If you are unsure which belt width, drive arrangement, or control interface fits your line, send us your requirements and we will recommend a layout and quote.
The safety obligations that sit around a powered conveyor - guarding, emergency stops and access - are the general machine-safety duties published by the US Occupational Safety and Health Administration. Where a specification names a test method for the equipment or its components, it is normally an ASTM International standard, and the measurement traceability behind any acceptance test rests on the framework published by NIST.